
Payload Management Systems: Preventing Overloads Without Slowing Production
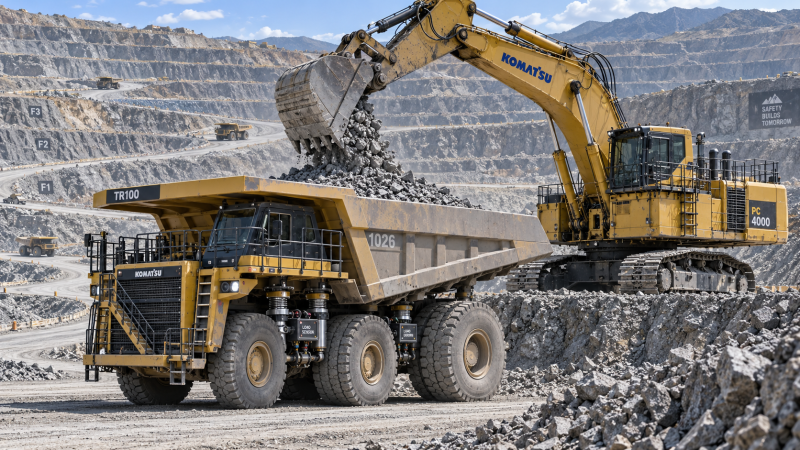
Overloads are rarely caused by a single obvious mistake. They often develop through small variations: wetter material, a different bucket fill pattern, a truck positioned on a side slope, an excavator working from a higher bench, or a loading target carried over from a previous material zone. A payload management system prevents these variations from turning into structural stress, tire damage, poor braking behavior, spilled loads, and avoidable rehandling while preserving the rhythm of the production cycle.
The practical aim is not to load every machine to the same displayed number. It is to place each load within a workable range that reflects the machine configuration, material density, haul route, body capacity, lift geometry, and site conditions. A reliable system turns load information into a timely decision at the point of loading, before an overfilled truck leaves the face or a lift proceeds beyond its planned limit.
Start with a payload target that reflects the actual task
A nominal rated payload is an important reference, but it is not a universal loading target. It describes a machine capability under defined assumptions. The usable target on a working site must account for how the machine is being used. A haul truck moving compacted rock on a dry, maintained route faces different loading constraints from the same truck carrying sticky overburden down a wet ramp with frequent stops. The scale may show an acceptable mass in both cases, yet the second duty cycle places greater demand on traction, braking, suspension, and tire temperature.
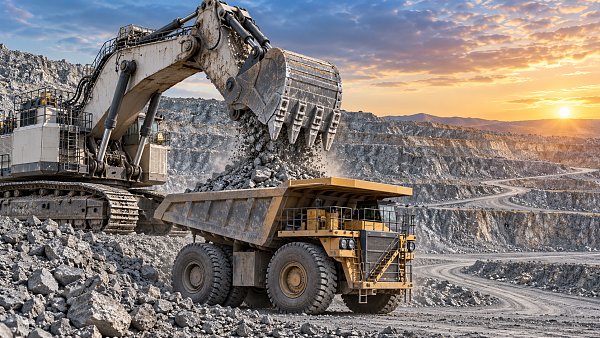
For excavators and loaders, the limiting condition may be bucket capacity, stability, breakout force, or truck-body volume rather than a simple mass value. Low-density blasted coal can fill a body before it approaches its mass target. Dense ore or wet clay can reach the mass limit with substantial apparent empty space remaining. Chasing a visually full body in the latter situation is a common route to overload.
Lift planning requires an even narrower distinction. A crane's available capacity changes with radius, boom length, boom angle, reeving, counterweight arrangement, ground bearing conditions, wind exposure, and the weight of all lifting accessories. The hook block, slings, spreader beam, rigging, and below-hook devices belong in the load calculation. Treating the component's stated weight as the payload understates the actual lifted load.
Use a defined operating band, not a single ideal number
A single exact target encourages correction after the fact: one pass too heavy is offset by one pass too light. That approach creates inconsistent machine loading and usually adds idle time. A target band gives loading equipment enough tolerance to work smoothly while still identifying a load that requires action. The band should be based on the planned payload and the uncertainty of the measurement method, not on the most optimistic reading available.
That distinction matters when a system measures payload through hydraulic pressure, axle strain, suspension pressure, load pins, or onboard scale cells. Each method responds differently to machine attitude, motion, temperature, boom position, and load distribution. A displayed value is useful only when its operating conditions are understood.
- Hydraulic-pressure estimates work well for rapid loader and excavator feedback, but the reading can shift when lift arms are accelerating, the machine is articulated, or the bucket is held at a different reference height.
- Truck-mounted systems reveal the final accumulated load, yet their value depends on correct calibration and a stable reading condition. Material can also shift inside the body after loading.
- Crane load-moment systems must be interpreted alongside radius and configuration data. A correct suspended-load reading does not override a configuration error.
Measure the load at the right moment
Fast production depends on getting a dependable reading without inserting a separate weighing ritual into every cycle. The best measurement point is the point at which a correction is still quick and safe. For a truck-loading excavator, that may be the final bucket pass before departure. For a wheel loader, it may be the lift phase used consistently for bucket payload estimation. For a crane, the load must be verified during the controlled initial lift, when the load is clear enough to confirm its behavior but before it is moved through the planned travel path.
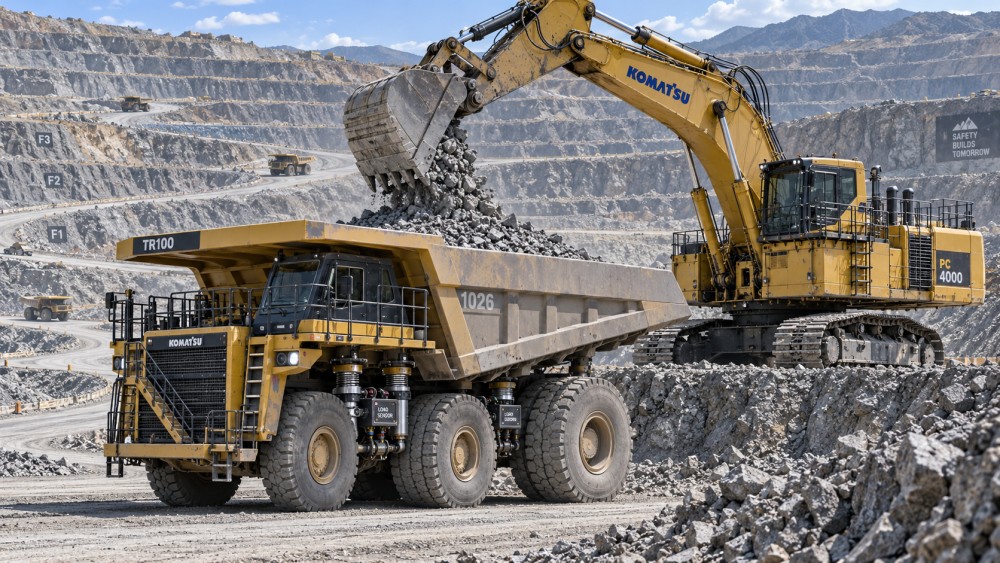
Readings gathered during travel, swing acceleration, hard braking, or active boom movement may fluctuate for reasons unrelated to actual payload. Filtering software can reduce noise, but filtering cannot repair an unstable measurement process. Establishing a repeatable reference position is usually more valuable than adding complexity. The bucket should be held at the same approximate height and machine posture for each payload calculation; truck readings should be taken under the site conditions specified for that system; lift instrumentation should match the active boom and reeving configuration.
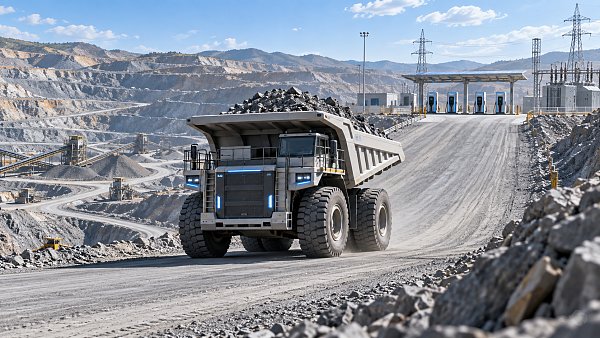
Load distribution deserves separate attention. A truck at the intended gross mass can still handle poorly if material is concentrated at one end of the body. Uneven placement changes axle loading, suspension behavior, and the way material leaves during dumping. A high central mound may also strike a canopy, conveyor, chute, or overhead structure that a level load would clear. In crane work, an off-center center of gravity can create rotation or side loading even when the total load weight is within plan.
Keep production moving through pass management
Most preventable overloads begin before the final pass. When the loading machine has no pass target, each bucket is judged by appearance and habit. Material fragmentation, bucket penetration, moisture, and operator technique then turn the final pass into a guess. Payload management becomes faster when the planned truck load is translated into an expected number of passes and an expected average payload per pass.
This does not require every bucket to carry identical mass. The first pass may be lighter because the bucket is trimming a face or building a stable base in the body. A later pass may be reduced to bring the accumulated value inside the target band. The useful question is whether the remaining capacity can accept a normal bucket, a trimmed bucket, or no additional material. Answering that question before the bucket is filled avoids dumping material back at the face or sending a truck away overloaded.
Material changes should trigger a reset of that expectation. Fragmented dry rock, fine wet material, frozen lumps, and mixed waste may occupy the same bucket very differently. A sudden rise in average bucket payload is not automatically improved digging performance. It may signal moisture uptake, denser geology, altered bucket fill, or a sensor bias. Likewise, a lower-than-expected bucket payload may come from poor fragmentation, spillage, tooth wear, a changed digging angle, or voids in the material.
Separate underload from low productivity
An underloaded truck is not always evidence of poor loading. If the body is volume-limited by low-density material, adding more passes may only create spillage and a high center of mass. If the truck is held at the loading point because the excavator is waiting for a clean face, the lost production is a queuing or diggability issue, not a payload issue. Correcting the wrong variable can make both problems worse.
The same distinction applies to a deliberately reduced load. A lower target can be appropriate when the haul road is soft, when a section of route has restricted traction, when a dump point is congested, or when material needs to be placed with controlled distribution. The decision should be visible in the shift plan rather than appearing as unexplained variance in the payload report.
Make alerts useful enough to act on
An alert that arrives too late, sounds too often, or gives no indication of severity will eventually be ignored. Payload notifications should match the available corrective action. A pre-limit indication during loading gives time to trim the next bucket. An overload indication after the final pass should make the next action unambiguous: remove material, redistribute it where appropriate, or hold the machine for review. A warning issued only after the truck has entered the haul road records the problem but does not control it.
Alert thresholds also need to account for measurement resolution. A system that repeatedly flags minor fluctuations around a limit encourages unnecessary adjustments. A system with a wide dead band can allow meaningful overloads to pass unnoticed. Stable measurements, sensible thresholds, and a clear escalation path matter more than a dashboard full of changing values.
Calibration is an operating discipline
Payload data loses value gradually. A machine may still display plausible numbers while drifting far enough to distort loading decisions. Mechanical wear, damaged wiring, hydraulic leakage, sensor movement, altered suspension characteristics, replacement components, and changes to tire size or pressure can all affect accuracy. Calibration should therefore follow events that change the measuring system, not merely a calendar interval.
Reference loads need to resemble the way the machine actually works. A static test conducted on level ground may confirm that a sensor responds, but it may not reveal errors introduced by working posture, bucket lift height, or body loading sequence. Validation across a representative payload range is more informative than confirming one point near the middle of the scale.
Data trends often reveal problems before a hard fault appears. A persistent difference between onboard payload and a controlled reference, a widening spread in bucket-pass values, or a repeating bias on one machine should be investigated. Do not automatically force the data to match by applying an offset. First determine whether the mismatch comes from the onboard system, the reference scale, material retention, incomplete unloading, or an inconsistent weighing position.
Protect the cycle, not just the machine
Payload control works best when loading, hauling, dumping, and maintenance observations are connected. A truck repeatedly loaded near the upper edge may show longer braking distances, higher tire stress, suspension events, or body damage. A loading unit with increasing bucket variation may be working in deteriorating material or developing linkage wear. These signals should feed back into the daily loading target and pass plan.
Short, specific handovers are more useful than broad reminders to avoid overloads. Record the active material, expected pass count, current target band, unusual road conditions, and any sensor concern that has not been resolved. This keeps the next shift from treating a temporary condition as normal performance.
Production speed is protected when each load is made correctly before dispatch, instead of corrected through spillage cleanup, rehandling, damaged equipment, or interrupted haulage. Accurate payload management creates that discipline by tying a stable measurement to the physical limits of the machine and the conditions of the work.
Related News
 Oct 11, 2026What Drives TBM Cutter Head Material Cost and Life-Cycle Value?Cutter head material cost explained: compare TBM alloys, wear protection, downtime risk, and life-cycle value to choose the most reliable, cost-effective solution.
 Oct 11, 2026Payload Management Systems: Preventing Overloads Without Slowing ProductionPayload management helps prevent overloads, protect equipment, and keep production moving. Learn how accurate targets, pass planning, alerts, and calibration improve every load.
 Oct 09, 2026Ultra-Large Excavator Bucket Size: Capacity, Width, and Site Fit ExplainedUltra large excavator bucket size explained: compare capacity, width, payload, truck matching, and site conditions to select a reliable, high-productivity bucket.
 Oct 08, 2026How to Evaluate a Heavy Machinery Information Platform for Project Equipment SourcingHeavy machinery information platform guide: compare equipment fit, source reliability, lifecycle costs, supplier capability, and compliance to make smarter sourcing decisions.
Heavy Haulage Strategist
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.