
How to verify equipment durability before approving suppliers at scale
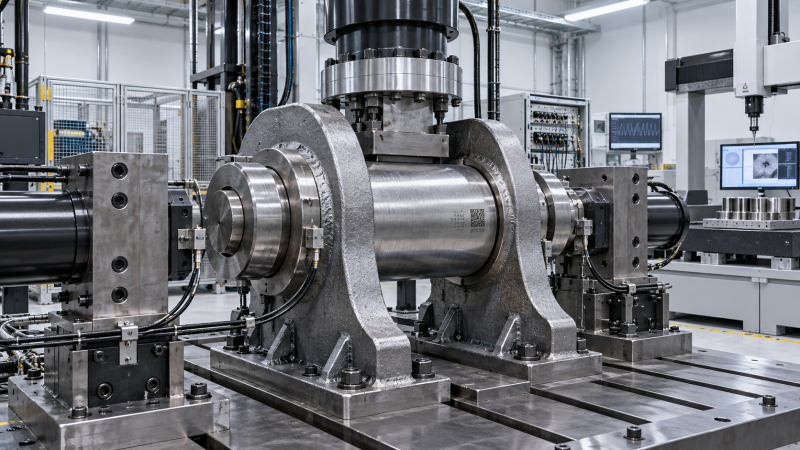
Durability approval should begin with a defined operating envelope, not a supplier certificate. A forged boom pin, TBM cutter-head component, excavator linkage, crane slew-ring fastener, or mining-truck suspension part can meet a drawing while failing early under the actual combination of load reversals, contamination, misalignment, temperature, vibration, and maintenance intervals. The approval record needs to show that the proposed part has been evaluated against those conditions and that the supplier can reproduce the validated condition in routine production.
Start by translating the equipment duty into measurable failure drivers. Static rated load is only one input. A structural weldment may see low nominal stress but severe local stress concentration at a bracket edge. A hydraulic cylinder rod may be structurally adequate yet lose service life through surface damage, inadequate coating adhesion, or abrasive contamination. A bearing housing can pass a proof-load test while its bore geometry shifts after heat treatment or repeated thermal cycles. The durability question must therefore be tied to the actual failure mode being controlled.
Set the evidence threshold before reviewing suppliers
A useful approval specification separates design capability from production capability. Design capability asks whether a part made to the proposed material, geometry, heat treatment, and process route can survive its intended duty. Production capability asks whether each delivered batch remains inside the conditions represented by that evidence. These are related but cannot be substituted for one another.
For critical components, the technical file should identify the load cases, expected life basis, environmental exposure, mating-part interfaces, permitted repair methods, inspection points, and rejection criteria. It should also state which changes require revalidation. A drawing revision is not the only meaningful change. A new steel mill, revised quench medium, different welding consumable, altered machining allowance, relocated coating line, or subcontracted heat-treatment operation can alter durability without changing the final part number.
Acceptance criteria need enough resolution to prevent a pass/fail result from hiding marginal performance. “No visible crack” after a test is weak evidence unless the loading spectrum, cycle count, inspection method, stress location, and part condition are documented. Equally, a tensile-test result from a separately cast coupon does not automatically establish properties in a thick forged section, beside a weld heat-affected zone, or after a production repair.
Trace material from source to installed condition
Material traceability has value only when the trace chain remains connected to the physical part. Heat number records, mill certificates, receiving inspection, cut-piece identification, machining travelers, and final serial marking should lead back to the same material lot. Where a component is assembled from several controlled items, such as a fabricated frame, cylinder, gearbox housing, or roller assembly, the record must preserve the identity of each safety-relevant input.
Review chemical composition and mechanical-property data in context. A material grade name alone says little about cleanliness, section-size effect, hardenability, grain condition, inclusion content, or actual heat-treatment response. For high-cycle loaded shafts and pins, surface condition and local hardness transitions can matter as much as bulk tensile strength. For castings, shrinkage, porosity, hot tears, and local wall-thickness changes require attention because a coupon may not represent the most heavily loaded region. For weldments, base metal, filler metal, joint preparation, preheat, interpass control, and post-weld treatment belong in the same evidence chain.
Positive material identification is particularly useful where alloy confusion would create a serious downstream consequence. It should be applied at a defined point in the process and linked to segregation controls, not treated as a ceremonial final inspection. A correct alloy piece placed in the wrong heat-treatment batch can still have unsuitable properties.
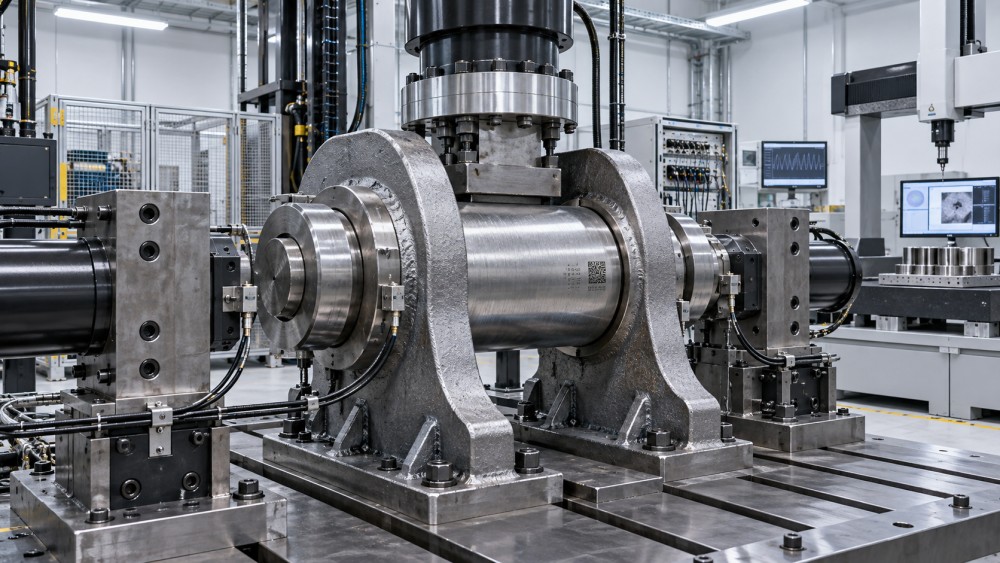
Traceability also needs to survive nonconforming events. If a batch is reworked, straightened, locally blended, weld-repaired, re-machined, or re-coated, the disposition record should state what was done, where it was done, and whether the original validation still applies. Unrecorded rework is a recurring source of misleading durability history because the delivered component no longer represents the tested process condition.
Use testing that reflects the governing damage mechanism
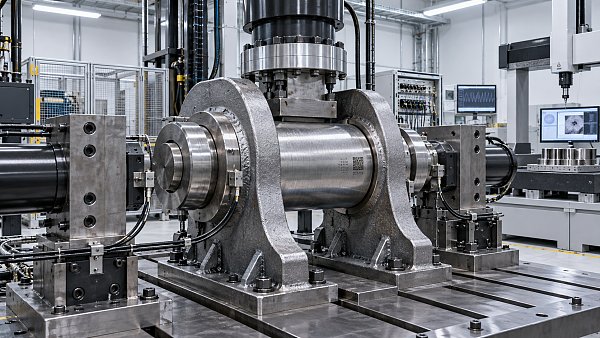
Durability verification is strongest when the test method is selected from a failure hypothesis. Fatigue cracks are driven by stress range, cycle sequence, mean stress, surface finish, residual stress, corrosion, and geometric discontinuities. Wear is driven by contact pressure, hardness pairing, abrasive particle size, lubrication state, and alignment. Structural buckling, seal extrusion, thread loosening, and hydraulic hose degradation each require different evidence. A generic endurance test may expose gross weakness while missing the mechanism that limits field life.
A test article must be representative in the ways that influence failure. Geometry, material heat, welding position, machining sequence, heat treatment, coatings, assembly preload, and boundary conditions can all matter. A prototype machined from billet may be unsuitable proof for a later casting. A carefully prepared laboratory weld may not represent a production joint made in a different fixture orientation. When full-scale testing is impractical, combine validated analysis with targeted physical testing of the critical feature, and document the assumptions that connect the two.
Load spectrum quality deserves close scrutiny. Repeating a constant load for many cycles can be useful for comparison, yet equipment in rock excavation, mine haulage, lifting, and road construction often experiences variable amplitude loading. Shock loads, reversals, off-axis loading, operator-induced transients, starts and stops, and transport vibration can accelerate damage differently from steady operation. The test rationale should explain whether these events are excluded, represented, or bounded by a conservative case.
Read field data without confusing exposure with durability
Field-performance evidence becomes persuasive when it is normalized. Raw warranty counts or return rates can mislead because one supplier's components may have accumulated far more operating hours, harsher payloads, different duty cycles, or better maintenance than another's. Link service records to serial or batch identity, installation date, operating hours, load environment where available, failure location, teardown findings, and corrective action.
Failure classification matters. A cracked mounting ear, a failed grease seal, and a seized bushing should not be grouped as a single “assembly failure.” The first may indicate stress concentration or weld quality; the second may point to contamination or seal geometry; the third may arise from lubrication access, clearance, or installation alignment. Grouping unlike failures makes a supplier history appear cleaner or worse than the engineering evidence supports.
Early failures deserve special handling because they often reveal production escape rather than wear-out behavior. A cluster from one serial range may trace to an incorrect heat-treatment cycle, missing surface treatment, an assembly fixture shift, or mixed material. That does not necessarily condemn the underlying design, but it does challenge process control. Conversely, a component that survives initial operation and fails only after a particular high-load duty may expose a validation gap even when factory records are orderly.
Audit the process that creates variation
A factory visit should follow the characteristics that govern durability instead of becoming a general housekeeping review. Walk the actual route from incoming material to packing. Confirm where part identity is assigned, how lots are segregated, which dimensions are measured before irreversible operations, and how inspection status is prevented from being overwritten. Observe the process at the shift, line, and subcontractor level relevant to the planned supply volume.
Special processes require deeper evidence because final inspection cannot reliably recover their output. Heat treatment, welding, coating, plating, shot peening, carburizing, nitriding, and controlled tightening can change fatigue performance or corrosion resistance while leaving a part visually acceptable. Review equipment calibration, recipe access control, furnace or bath loading discipline, qualification of operators, recorded parameters, sample locations, and handling after the process. A test result is less credible when the supplier cannot show that production parts received the same thermal cycle, surface preparation, or treatment intensity as the tested article.
Measurement-system capability must be considered alongside reported dimensions. A bore gauge used inconsistently, a hardness method unsuitable for a thin hardened layer, or a torque tool with unverified response can produce reassuring records without controlling the characteristic. Attribute inspections are especially limited near a specification boundary. When a small change in diameter, coating thickness, runout, or preload has a large effect on life, variable data and an understood measurement method are needed.
Approve a controlled configuration, not a supplier name
Scaled approval works best when the approved object is a controlled configuration: part revision, manufacturing site, process route, approved sub-tier sources, inspection plan, and evidence set. This approach makes it possible to distinguish a mature production route from a similar-looking alternative that has not earned the same durability confidence.
Risk can then be tiered by consequence and uncertainty. A component whose failure could cause loss of load control, structural separation, braking impairment, fire exposure, or uncontrolled motion warrants stronger traceability, more representative validation, and tighter change notification than an easily replaceable, non-safety-critical cover. The method should also account for detection opportunity. A part that can be routinely inspected before damage becomes hazardous is different from an internal component that offers little warning.
- Release evidence: retain the test basis, drawings, material and process records, inspection results, and deviations that define the accepted configuration.
- Change gates: require advance review for changes to source material, manufacturing location, special process, tooling that affects critical geometry, or critical sub-tier supply.
- Ongoing verification: use receiving data, periodic process review, targeted lot testing, and field returns to test whether production remains aligned with the approved condition.
- Escalation logic: define what triggers containment, additional sampling, root-cause investigation, revalidation, or temporary suspension of release.
Supplier resilience belongs in the same approval decision because a technically capable facility can still create durability exposure through uncontrolled substitution, capacity pressure, weak sub-tier visibility, inadequate preservation during transport, or poor response to nonconformities. Review how shortages are handled, who can authorize deviations, whether alternate sources are prequalified, and how affected serial ranges can be identified after shipment. The purpose is not to eliminate every disruption; it is to ensure that disruptions do not silently change the verified product.
Close the loop through failure analysis
When a durability-related event occurs, preserve the component and its records before repair or disposal obscures the evidence. Record installation orientation, mating parts, lubrication state, visible damage, torque marks where relevant, service exposure, and serial identity. A laboratory result without operating context can identify fracture features yet still miss the initiating condition.
Corrective action should be tested against the original failure mechanism. Increasing hardness may reduce abrasive wear while worsening brittleness or fatigue sensitivity. Adding weld metal can restore section size while introducing residual stress and a new crack initiation site. Raising torque can improve clamp load only if friction and joint behavior are controlled. Closeout is justified when the causal chain, containment scope, revised control, and verification evidence agree; a statement that the issue has been “addressed” is not durability evidence.
The durable supplier relationship is built from this repeatable chain: defined duty, traceable material and process history, representative validation, production surveillance, and disciplined response when reality differs from the approval file. That record supports release decisions at scale while keeping the focus on the condition that matters most: whether delivered equipment will withstand its intended service without hidden variation entering the fleet.
Related News
 Sep 29, 2026Infrastructure Construction Standards: A Project Manager’s Guide to ComplianceInfrastructure construction standards guide for project managers: turn requirements into field controls, hold points, traceability, and compliant delivery.
 Sep 28, 2026How to Specify Custom Mining Equipment for Abrasive Ground and High-Load HaulageCustom mining equipment for abrasive ground and high-load haulage: learn how to optimize payload, wear protection, powertrains, uptime, and lifecycle cost for safer, reliable production.
 Sep 29, 2026What belongs in a construction equipment package sourcing plan?Construction equipment package planning sourcing guide: learn how to match machines, attachments, site conditions, supplier support, costs, and acceptance gates for reliable project delivery.
 Sep 29, 2026How to verify equipment durability before approving suppliers at scaleHow can heavy equipment manufacturers verify durability and manage supplier risk at scale? Explore practical testing, traceability, audits, and control strategies.
Ms. Elena Rodriguez
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.